Unlocking High Hardness Gear Cutting with Negative Rake Angles
author: Cash
2026-06-15
Hard Carbide Hobs vs. HSS: Unlocking High-Hardness Gear Cutting with Negative Rake Angles | Gearseiko
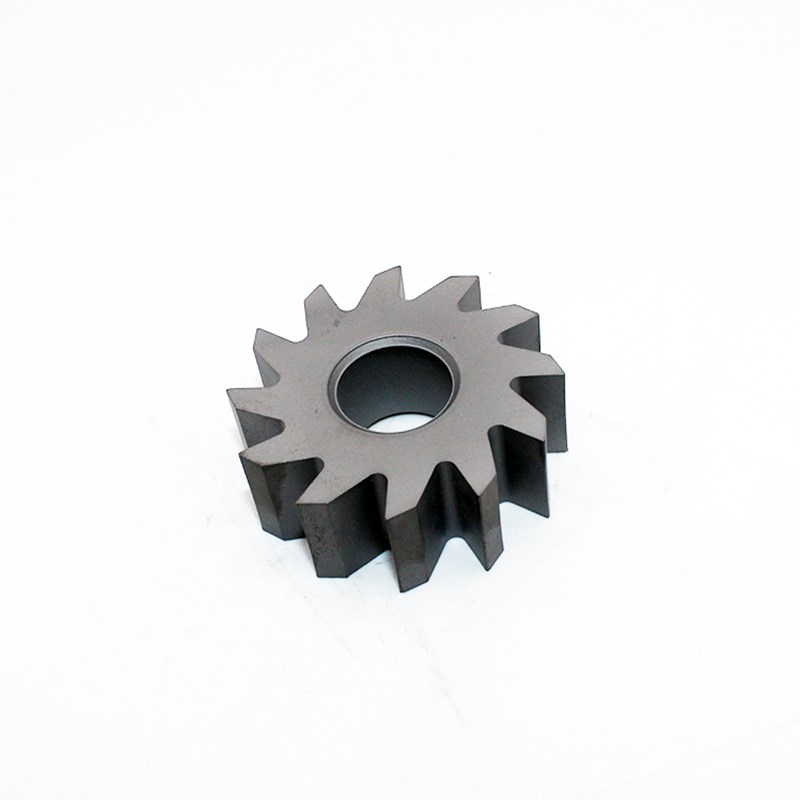
Conventional high-speed steel (HSS) hobs hit performance limits when machining high-hardness gear components. For manufacturers pursuing superior precision, tool durability and production efficiency in hard gear hobbing, solid carbide hobs have become a transformative solution. Specializing in high-end precision gear manufacturing, Gearseiko has in-depth expertise in carbide hob cutting properties, pushing the technical boundaries of modern gear machining.
Core Challenge: Brittleness of Carbide in Interrupted Cutting
Carbide hobs feature outstanding hot hardness and wear resistance, outperforming HSS hobs drastically and enabling the machining of hardened materials beyond the capacity of HSS tools. Nevertheless, carbide materials come with an inherent drawback: lower toughness.
Gear hobbing is a typical interrupted cutting process. Each hob tooth repeatedly makes and breaks contact with the workpiece, and carbide brittleness greatly raises risks of edge chipping and tool breakage. This issue has long restricted the wide adoption of carbide hobs in hardened gear finishing.
Effective Solution: Radial Large Negative Rake Angle Design
To tackle the above problem, Gearseiko adopts a specialized geometry design — large radial negative rake angle for solid carbide hobs. This design revolutionizes cutting mechanics, reinforces cutting edge toughness, and makes reliable hard gear hobbing achievable.
Technical Comparison: Zero Rake vs. Large Negative Rake
-
Zero rake hob (0°) The radial rake face stands perpendicular to the cutting direction. The entire side cutting edge engages the workpiece almost at the same time, generating heavy impact loads. It produces fragmented chips, triggers frequent micro-chipping and shortens overall tool life.
-
Large negative rake hob (-20° to -30°) The rake face forms an acute angle against the cutting direction. Cutting starts from the root of the side edge and gradually extends toward the tip, forming an oblique scraping action. Such tools are also known as scraping hobs, and the process is called scraping hobbing. This design eases impact force, distributes cutting load across a longer edge and generates continuous spiral chips.
Major Advantages of Gearseiko’s Negative Rake Carbide Hobs
- Reduced cutting vibration: Gentle oblique cutting minimizes chatter and delivers superior surface finish on hardened gear flanks.
- Improved edge toughness: Lower impact effectively prevents chipping and sudden breakage, even for machining hardened steel ranging from 50–62 HRC.
- Smooth chip removal: Continuous spiral chips avoid flute clogging and jamming between edge and workpiece, eliminating a main cause of tool damage.
- Slower flank wear: Cutting force spreads over a longer working edge, slowing down wear progression, extending tool life and stabilizing gear accuracy during long-run production.
Selection of Optimal Negative Rake Angle
The ideal rake angle is determined by gear module. Larger negative angles boost cutting performance yet increase manufacturing difficulty and affect tooth profile precision, requiring balanced design.
Referring to mature standards from top manufacturers, Gearseiko follows the guidelines below for solid carbide hobs:
- Module m ≤ 2.0 mm: Recommended rake angle -25° ~ -30°
- Module m > 2.0 mm: Recommended rake angle -15° ~ -20° for balanced cutting performance and profile accuracy
We also provide fully customized hob geometry based on actual material hardness, gear module and machine conditions. Our team conducts professional cutting simulation and on-site verification to determine the most suitable rake angle for your working conditions.
Why Partner with Gearseiko for Hard Gear Hobbing?
More than just tool supply, Gearseiko delivers complete integrated machining solutions. Our negative rake solid carbide hobs bring prominent values:
- Support hard hobbing as the final finishing process, cutting down or even eliminating grinding procedures.
- Stably achieve DIN 5 ~ DIN 6 accuracy for pre-hardened and fully hardened gears.
- Achieve 2–3 times longer service life compared with standard carbide hobs and coated HSS hobs for hard cutting scenarios.
With profound know-how in hob geometry, especially large negative rake design, we help you safely replace grinding with hard hobbing, cutting production time and costs while retaining high product quality.
Conclusion
Solid carbide hobs enable efficient high-speed machining of hardened gears, while carbide brittleness remains a key hurdle to overcome. The large radial negative rake angle is the core solution, creating low-impact oblique scraping cutting.
Gearseiko has fully mastered this design technology, producing carbide hobs that combine excellent wear resistance, reliable edge toughness and high precision. Whether you plan to upgrade from HSS tools to carbide hobs or optimize existing carbide cutting performance, feel free to contact us. We will customize the best rake angle solution to maximize your production benefits.
FAQ | Negative Rake Carbide Hobs & Hard Gear Cutting
Q1: What is the main weakness of carbide hobs in gear hobbing?
A1: Carbide has low toughness. Interrupted cutting causes impact load, easily leading to edge chipping and breakage.
Q2: How does large negative rake angle improve cutting performance?
A2: It creates oblique scraping action, reduces impact force, optimizes chip formation and enhances edge toughness.
Q3: What are the recommended rake angles for different gear modules?
A3: -25°~-30° for module ≤2.0 mm; -15°~-20° for module over 2.0 mm.
Q4: What HRC range of hardened steel is applicable for our negative rake carbide hobs?
A4: Suitable for hardened steel with hardness between 50 HRC and 62 HRC.
Q5: What benefits can users get by adopting Gearseiko’s carbide hobs?
A5: Higher gear accuracy, 2–3x longer tool life, less grinding work and lower overall production cost.
5 Core Requirements for Gear Hobbing Machines
Gearseiko Leads the Efficient Hard Hobbing Era
Related Article