Unlocking Cost Effectiveness and Efficiency in High Precision Gear Manufacturing
author: Cash
2026-06-17

Carbide Hobbing: Unlocking Cost-Effectiveness and Efficiency in High-Precision Gear Manufacturing | Gearseiko
In the high-end precision gear manufacturing industry, gear grinding has long been the mainstream finishing process for hardened gears. Nevertheless, gear manufacturers are constantly plagued by multiple bottlenecks including expensive grinding machine investment, low material removal efficiency, and continuously rising labor and production costs. As an innovative alternative process, carbide hard hobbing brings disruptive optimization to traditional gear manufacturing workflows. Whether applied as direct finishing replacement for gear grinding or as an efficient semi-finishing pre-process before fine grinding, carbide hobbing delivers prominent efficiency improvement and overall cost reduction for modern gear production lines.
Core Economic Value: Replace or Optimize Traditional Gear Grinding Processes
Carbide hobbing creates dual economic benefits for gear factories: direct grinding replacement for medium-precision gears, and grinding load reduction for ultra-high-precision gears, covering all mainstream hardened gear production scenarios.
1. Direct Grinding Replacement for ISO 7–Grade Hardened Gears
For hardened gears with precision requirements of ISO Grade 7 and below, high-precision carbide finish hobbing can completely replace conventional gear grinding as the final finishing procedure. Featuring ultra-high hardness and outstanding wear resistance, solid carbide hobs support stable high-speed cutting on hardened workpieces ranging from 45 HRC to 64 HRC. In actual mass production, its machining efficiency is 5–6 times higher than traditional bevel gear grinding machines, while overall production costs drop significantly.
Industry data verifies that carbide hard hobbing cuts comprehensive manufacturing costs by 20%–60% compared with full grinding processes. A classic mass production case from Ford Motor Company fully proves its practical advantages: dry carbide hobbing reduces machining cost by 44%, shortens overall production cycle time by 48%, and extends average tool service life by 6 times compared with original grinding processes.
2. Semi-Finishing Pre-Hobbing for ISO 3–6 High-Precision Gears
For high-precision gears within ISO Grade 3 to Grade 6 that require final grinding, carbide semi-finish hobbing acts as an essential pre-process after heat treatment. Carburizing and quenching inevitably cause irreversible tooth profile distortion and dimensional deviation on gear blanks. Direct feeding distorted gears into grinding needs large grinding stock allowance, prolonged grinding cycle time, and brings high risks of grinding burn and surface thermal damage.
Adding one carbide semi-finish hobbing procedure after heat treatment efficiently removes overall heat treatment distortion, leaves uniform and minimal finishing allowance for subsequent grinding. This optimized composite process saves 50% to more than 80% grinding time, showing particularly outstanding cost and efficiency advantages for large-module and large-diameter hardened gears that are difficult and time-consuming to grind.
Inherent Technical Advantages: Tool Material Upgrade & Optimized Cutting Mechanics
All cost and efficiency benefits of carbide hobbing originate from upgraded tool material performance and optimized cutting mechanism, far surpassing traditional HSS (high-speed steel) hobbing:
-
Excellent high-temperature resistance: Solid carbide hobs withstand extreme cutting heat and periodic impact loads during dry cutting. The maximum cutting speed reaches 260 m/min, while conventional HSS hobs only support 90–160 m/min. Higher cutting speed greatly improves machine tool utilization and hourly output.
-
Optimized micro-extrusion cutting mechanism: Different from conventional cutting methods, carbide hard hobbing adopts mild micro-extrusion cutting. It polishes gear tooth profiles subtly, improves flank surface integrity, enhances overall tooth root bending strength, and restrains surface fatigue crack initiation. Accordingly, finished gears gain longer service life and better fatigue resistance.
-
Lower follow-up processing difficulty: Uniform residual allowance after carbide pre-hobbing stabilizes grinding processing status, reduces frequent parameter debugging, and lowers the defective rate caused by uneven grinding stock.
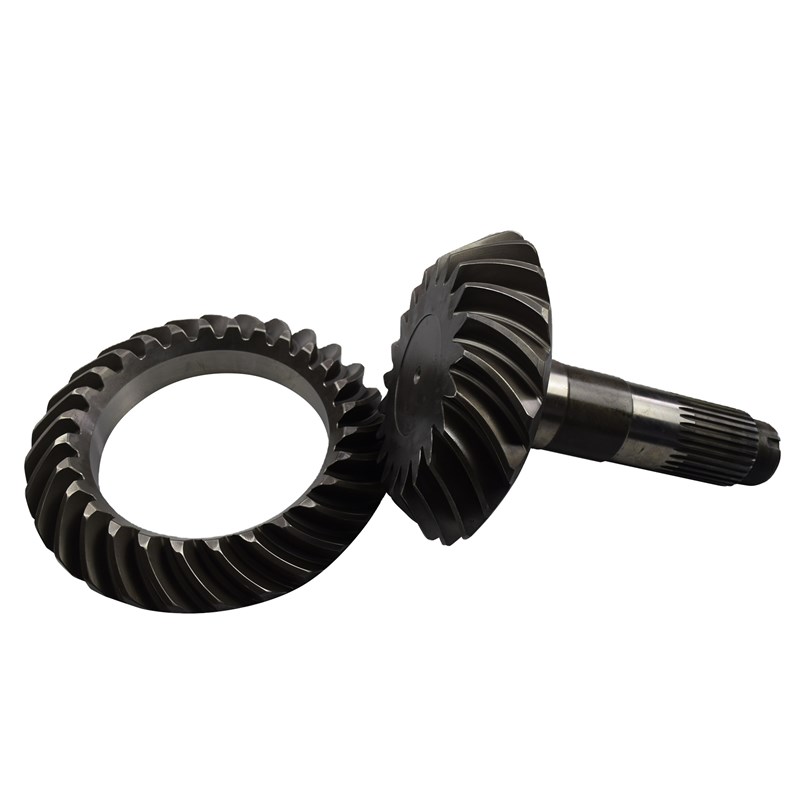
Gearseiko Customized Process Solutions for Different Precision Grades
Facing increasingly fierce global gear manufacturing competition, cost control, stable precision and fast delivery are three core competitive indicators for gear suppliers. Equipped with high-rigidity CNC hobbing machines and high-performance customized solid carbide hobs, Gearseiko matches exclusive process routes targeting different gear precision standards:
-
ISO Grade 6–7 Medium-precision hardened gears: Process route — Hobbing → Heat Hardening → Carbide Finish Hobbing. Eliminate grinding procedures completely, guarantee qualified precision with the lowest production cost and shortest lead time.
-
ISO Grade 3–6 Ultra-high-precision hardened gears: Process route — Hobbing → Heat Hardening → Carbide Semi-finish Hobbing → Precision Grinding. Remove most heat treatment distortion in advance, sharply cut grinding workload, avoid grinding burn defects, and maintain ultra-high finished gear precision.
Closing Remarks
Carbide hobbing is not merely a simple tool replacement, but a revolutionary process upgrade for the entire hardened gear manufacturing chain. It solves long-standing pain points of high cost, low efficiency and high defect risks of traditional grinding processes. Gearseiko insists on applying mature carbide hobbing technology to mass production, helping global customers shorten delivery cycles, cut manufacturing expenditure and maintain long-term stable gear quality.
Every gear counts, every process optimization creates greater value for your production line.
FAQ | Carbide Hobbing Process, Cost & Application
Q1: Can carbide hobbing fully replace gear grinding?
A1: Yes. It can directly replace grinding for ISO 7 grade and lower hardened gears to cut cost greatly. For ISO 3–6 high-precision gears, it works as high-efficiency semi-finishing pre-process to reduce grinding workload instead of full replacement.
Q2: How much production cost can carbide hobbing save?
A2: Overall manufacturing cost can be reduced by 20%–60% compared with full grinding process. Ford’s practical case proves 44% machining cost reduction and 48% shorter cycle time via dry carbide hobbing.
Q3: What is the maximum cutting speed of solid carbide hobs?
A3: Solid carbide hobs support a maximum cutting speed up to 260 m/min under dry cutting conditions, much higher than 90–160 m/min of traditional HSS hobs.
Q4: Why add carbide semi-finish hobbing before grinding?
A4: It removes heat treatment distortion uniformly, minimizes grinding allowance, saves over half grinding time, and effectively avoids grinding burn and thermal damage on gear tooth flanks.
Q5: What are the advantages of carbide hobbing on gear performance?
A5: Its micro-extrusion cutting improves tooth flank surface quality, enhances tooth root strength, restrains fatigue cracks and prolongs the overall fatigue service life of finished gears.
Achieving Higher Efficiency at Lower Cost for Hardened Gear Machining
Gearseiko Helps Precision Gear Machining Reach New Heights
Related Article